Unplanned equipment failure is one of the costliest problems in chemical and petrochemical plants. A single failed pump or compressor can stop a process line, create safety risks, and delay shipments. The repair bill is only part of the loss. Off-spec product, emergency labor, and lost throughput add up quickly.
That is why petrochemical predictive maintenance is gaining ground across the USA and Europe. Instead of waiting for a breakdown or following a fixed calendar, teams use equipment data to spot problems early. Predictive maintenance software turns that data into clear alerts and practical maintenance plans.
This guide explains how it works, where it applies, and how to choose the right solution.
What Is Petrochemical Predictive Maintenance?
Petrochemical predictive maintenance uses real-time and historical equipment data to forecast failures before they happen. It helps teams service assets at the right time, not too early and not too late.
The difference from preventive maintenance is simple:
- Preventive maintenance follows a fixed schedule, such as servicing a pump every six months.
- Predictive maintenance follows actual condition. The pump is serviced when its data shows real wear.
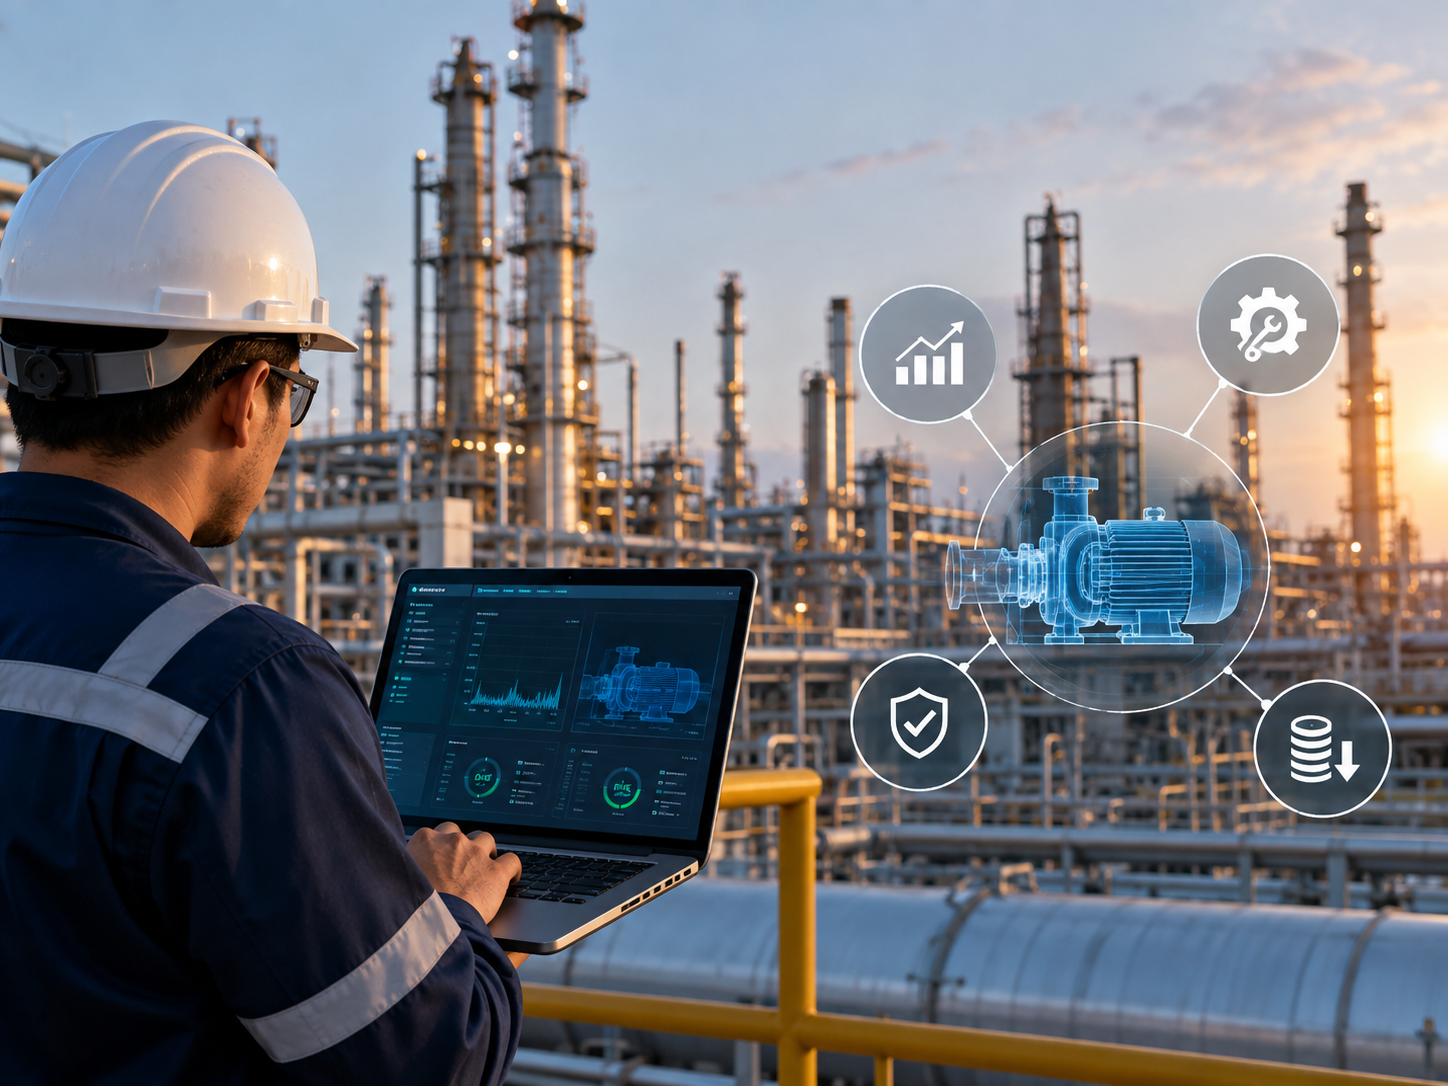
Fixed schedules can lead to unnecessary work on healthy equipment. They can also miss faults that develop between service dates. Sensors close that gap by tracking vibration, temperature, pressure, current, and flow. Combined with process data, these signals show how each asset behaves over time. Maintenance decisions then rest on evidence, not assumptions.
How Predictive Maintenance Software Works
Most platforms follow the same six-step flow:
- Data collection: Sensors, PLCs, DCS systems, and historians feed equipment data into one platform.
- Condition monitoring: Dashboards show the live health of each asset.
- Data analytics: The software builds a normal baseline for every machine.
- Anomaly detection: Deviations from that baseline are flagged automatically.
- Predictive alerts: Teams receive early warnings, ranked by risk.
- Maintenance planning: Alerts convert into work orders and planned outage tasks.
This flow moves teams from reacting to failures toward planning around them.
Common Equipment Applications
Industrial predictive maintenance covers most critical assets in a plant. Typical applications include:
- Pumps: Track vibration, seal condition, cavitation, and flow.
- Compressors: Watch bearing temperature, discharge pressure, and efficiency.
- Motors: Monitor current, winding temperature, and imbalance.
- Turbines: Detect shaft misalignment and performance drift.
- Heat exchangers: Identify fouling through temperature and pressure trends.
- Rotating equipment: Catch bearing wear and looseness early.
- Valves: Flag sticking, leakage, and slow response.
Pumps are often the best starting point because plants have many of them and they fail often. Solutions such as Xpump focus on this equipment class.
How Predictive Maintenance Reduces Equipment Downtime
Downtime falls when problems are found early and handled on your schedule.
- Early detection of abnormal conditions: Small changes in vibration or temperature often appear well before failure.
- Faster fault identification: Analytics point to the likely cause, so technicians spend less time troubleshooting.
- Better maintenance scheduling: Repairs move into planned turnarounds instead of emergency stops.
- Fewer unplanned shutdowns: Developing faults are corrected before they force a trip.
In continuous process plants, avoiding even one unplanned stop can protect significant production value.
How Predictive Maintenance Reduces Maintenance Costs
Cost savings come from doing the right work at the right time.
- Condition-based maintenance: Work is triggered by asset health, not the calendar.
- Less unnecessary maintenance: Healthy equipment is left alone, which saves labor and parts.
- Better spare-parts planning: Early warnings give purchasing time to order parts without rush fees.
- Improved equipment utilization: Assets stay in service longer between interventions.
- Longer operating life: Fixing small issues early prevents secondary damage.
Together, these gains lower both direct repair costs and hidden production losses.
Role of AI in Predictive Maintenance
AI predictive maintenance extends basic monitoring with machine learning. Fixed alarm limits work for simple cases. They struggle when normal behavior changes with load, feed, or season.
AI-based predictive maintenance addresses this in four ways:
- Pattern recognition: Models learn how healthy equipment behaves across operating modes.
- Anomaly detection: Subtle deviations are flagged even when no alarm limit is crossed.
- Predictive analytics: Trends estimate how a fault may progress.
- Equipment health monitoring: Each asset receives a clear health status.
The result is maintenance insight that engineers can act on quickly. Engineers still make the final call. AI supports their expertise and does not replace it.
Predictive Maintenance Analytics for Chemical Plants
Predictive maintenance analytics brings several data layers together:
- Equipment health data: Vibration, temperature, and pressure readings.
- Historical trends: Patterns that reveal slow degradation.
- Real-time monitoring: Fast detection of sudden changes.
- Performance analysis: Comparison of similar assets across units.
- Maintenance alerts and reports: Summaries for daily and monthly reviews.
For teams using chemical manufacturing software, this means one clear view of asset condition instead of scattered spreadsheets. Reliability engineers can study trends, and managers can prioritize spending. Explore our predictive maintenance solutions to see how this works in practice.
Choosing Predictive Maintenance Software
Use these criteria when you compare predictive maintenance solutions:
- Industrial equipment connectivity: Support for common protocols and your existing sensors.
- Real-time data collection: Continuous, reliable data streaming.
- Analytics capabilities: Both rule-based and AI models.
- Scalability: Room to add assets without redesign.
- Integration with existing systems: Links to CMMS, ERP, DCS, and historians.
- Alerts and reporting: Clear, prioritized notifications and useful reports.
- Multi-asset and multi-site support: One platform across units and locations.
Also confirm that the vendor understands hazardous areas and continuous operation. Learn more about our work in the chemical and petrochemical industry.
Conclusion
Petrochemical predictive maintenance gives plants a practical way to improve equipment reliability, plan maintenance, and raise operational efficiency. Predictive maintenance software detects faults early, cuts unplanned downtime, and reduces avoidable maintenance spend. AI and analytics make those insights faster to act on.
eInnoSys helps chemical and petrochemical teams put this into practice with connected, data-driven solutions. To protect critical pumps and rotating assets, explore Xpump and see how predictive maintenance can support your plant.


